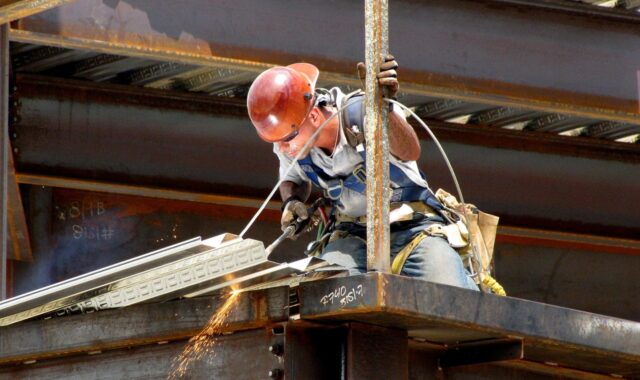
Health and safety systems for industrial equipment operations
Why health and safety systems matter for equipment-intensive work
Health and safety systems are more than a binder, a set of warning signs or an annual training file. In industrial equipment operations, they provide the structure for identifying hazards, selecting controls, training workers, checking performance and improving after changes or incidents. OSHA’s Recommended Practices describe safety and health programs as proactive, built to find and fix hazards before injury or illness occurs. ISO 45001 frames the same concept as an occupational health and safety management system with requirements for leadership, worker participation, planning, support, operation and improvement.
For equipment-intensive workplaces, the practical test is direct: can the system connect risk assessments, machine safeguarding, lockout procedures, maintenance, contractor work and incident learning into one repeatable process? If those parts operate separately, the site may have safety activities, but not a dependable management system.
The need remains visible in public injury data. In a January 22, 2026 release, the U.S. Bureau of Labor Statistics reported that private industry employers recorded 2.5 million nonfatal workplace injuries and illnesses in 2024, down 3.1 percent from 2023. In a February 19, 2026 release, BLS reported 5,070 fatal work injuries in the United States in 2024, with transportation incidents, falls, harmful exposures and violence among the major event categories. These figures do not identify what any single plant must fix, but they show why industrial organizations need systems that do more than respond after an event.
For more industrial content on protective controls, monitoring and operational risk, see the site’s safety systems category.
The core elements of an effective system
A strong program combines management responsibility, worker input, hazard analysis, engineering controls, training, measurement and improvement. Legal duties vary by country, state and industry, but the operating logic is similar across many recognized frameworks.
Management leadership and defined accountability
Leadership is the starting point because equipment safety often competes with production pressure, maintenance downtime, capital budgets and schedule changes. A credible system assigns clear responsibilities for risk assessment, corrective actions, machine guarding, lockout/tagout, emergency readiness and contractor coordination. It also gives supervisors enough time and authority to stop unsafe work, escalate hazards and verify that fixes were completed.
For industrial equipment sites, accountability should be linked to decisions that shape risk: purchasing machinery, modifying controls, bypassing interlocks for troubleshooting, approving maintenance procedures and restarting equipment after repair. If responsibility sits only with the safety department, the system will be weak because many serious hazards are created or controlled by engineering, operations, procurement and maintenance decisions.
Worker participation and reporting channels
OSHA’s safety management guidance emphasizes meaningful worker participation because operators, mechanics, cleaners and contractors often see hazards before management does. A useful system gives workers practical ways to report hazards, near misses, blocked guards, damaged sensors, unstable loads, recurring jams, ergonomic strain and unclear procedures. Reporting should not be treated as a sign of failure. It is one of the main inputs that allows a site to correct weak controls before an injury occurs.
Participation also means involving workers when job hazard analyses, standard work instructions and lockout steps are written or revised. A procedure created without the people who perform the task may look complete on paper but miss access constraints, visibility limits, awkward body positions or informal workarounds that occur during real production.
Hazard identification and risk assessment
Risk assessment is the bridge between general safety policy and specific controls. EU-OSHA describes risk assessment as a systematic examination of what could cause harm, whether hazards can be eliminated and what preventive or protective measures are needed. In an equipment environment, that assessment should cover normal production, cleaning, tool changes, clearing jams, maintenance, commissioning, abnormal operation, energy isolation, software changes and decommissioning.
Useful inputs include incident records, near miss reports, maintenance history, manufacturer information, safety data sheets, exposure monitoring, operator feedback, inspection findings and applicable standards. The assessment should be revisited when equipment is modified, production volume changes, a new material is introduced, a contractor performs unfamiliar work or an incident shows that earlier assumptions were wrong.
Education, training and competence checks
Training is often overused as a control and underused as a verification tool. A health and safety system should define which tasks require competence, what the person must know, how competence will be demonstrated and when refresher training is needed. For industrial equipment, this may include machine-specific startup and shutdown, authorized lockout/tagout, energized troubleshooting limits, confined space entry, powered industrial truck operation, lifting operations, chemical handling and emergency response.
The most useful training records do not simply prove attendance. They show that the worker can perform the task safely, understands the limits of the equipment and knows when to stop work and ask for help.
How controls connect the system to physical equipment
A safety management system becomes real when it affects the design, operation and maintenance of equipment. NIOSH’s hierarchy of controls is a useful decision model because it ranks control approaches from more reliable to less reliable. Elimination and substitution sit above engineering controls, administrative controls and personal protective equipment. In practice, a site may need several layers, but the system should avoid relying on PPE or memory when a stronger engineering or design control is feasible.
| Risk area | Preferred system response | Evidence to look for |
|---|---|---|
| Unexpected startup during service | Energy isolation, lockout steps, verification and authorization | Machine-specific procedures, training records, periodic audits and corrected findings |
| Contact with moving parts | Guarding, interlocks, safe distance, presence sensing and controlled access | Guard inspection logs, change records and documented approval for any temporary removal |
| Dust, fumes or chemical exposure | Substitution where feasible, enclosed process, local exhaust ventilation and exposure monitoring | Assessment records, ventilation maintenance, monitoring results and corrective action tracking |
| Manual handling and repetitive work | Mechanical assistance, layout changes, workstation design and job rotation where needed | Ergonomic assessments, operator feedback and injury trend review |
| Contractor maintenance | Pre-job briefing, permit controls, isolation coordination and supervision | Contractor qualification, permits, communication records and post-job review |
The table is only useful if it reflects the site’s actual work. The key is the connection between identified hazards, selected controls and evidence that those controls still function. A guard that exists on a drawing but is routinely removed during cleaning is not an effective control. A lockout procedure that has not been tested against the actual machine layout may fail when a mechanic encounters stored pneumatic, hydraulic, thermal or gravity energy. See also: production equipment.
Standards and public sources that help structure decisions
Industrial sites often use more than one reference source. Some references are legal or regulatory, some are voluntary standards and others are statistical or technical sources. They should not be treated as interchangeable.
| Reference source | What it contributes | Practical use in a health and safety system |
|---|---|---|
| OSHA Recommended Practices | A seven-element program model covering leadership, worker participation, hazard identification, prevention and control, training, evaluation and contractor coordination | Useful for building or reviewing a proactive workplace program, especially in U.S. settings |
| ISO 45001:2018 | Requirements for an occupational health and safety management system | Useful for organizations that want a formal, auditable management system or integration with other management standards |
| ISO 45001:2018 Amendment 1:2024 | Climate action changes requiring organizations to consider whether climate change is a relevant issue for the management system | Relevant when heat, severe weather, supply disruption or emergency planning could affect worker safety and system objectives |
| NIOSH hierarchy of controls | A risk control model ranking more reliable controls above less reliable ones | Useful when choosing between redesign, guarding, procedures, training and PPE |
| BLS injury and fatality data | National statistical context for nonfatal and fatal work injuries | Useful for benchmarking, trend awareness and prioritizing deeper review, but not a substitute for site-specific assessment |
ISO certification, where used, should not be mistaken for automatic legal compliance. A certified system can still miss a local regulatory requirement, a machine-specific hazard or a weak field practice. Conversely, a smaller organization without certification can still build a disciplined program if it defines responsibilities, assesses hazards, controls risk and reviews performance honestly.
Metrics that show whether the system is working
Many organizations track recordable injuries, lost time cases and total recordable incident rates. These lagging indicators are useful, but they mainly describe what has already happened. They can also move slowly on small sites, where a single case may change the rate sharply. A stronger health and safety system balances lagging indicators with leading indicators that show whether risk controls are being maintained.
- Corrective action closure quality: not only whether actions closed on time, but whether the fix addressed the root cause.
- Critical control verification: checks that guards, interlocks, ventilation, emergency stops and isolation points work as intended.
- Near miss and hazard reporting: reviewed by quality and follow-up, not by volume alone.
- Preventive maintenance completion: especially for safety-related devices and equipment that controls exposure.
- Training effectiveness: observed task performance, not just attendance.
- Management of change review: percentage of equipment, process or material changes reviewed before implementation.
- Contractor control performance: pre-job planning, permit quality, supervision and post-job learning.
The best metric set is small enough to be used and specific enough to guide action. If every monthly review produces the same generic message, the system is probably measuring activity rather than risk reduction.
A practical implementation roadmap
Organizations do not need to build every element at once. OSHA’s recommended approach encourages starting with a basic program and improving it over time. For equipment-heavy operations, a phased roadmap can reduce complexity while still addressing serious hazards early.
- Map the work: list equipment, tasks, energy sources, materials, work areas and contractor activities.
- Identify critical risks: focus first on hazards with severe potential outcomes, such as crushing, falls, hazardous energy, confined spaces, combustible dust, chemical exposure and vehicle interaction.
- Verify existing controls: inspect whether controls are present, functional, understood and used during real work.
- Close high-risk gaps: prioritize engineering and isolation controls before relying on signs, reminders or PPE.
- Standardize procedures: write task-specific instructions for startup, shutdown, cleaning, jam clearing, maintenance and abnormal conditions.
- Train and observe: confirm that people can perform the work safely under normal operating pressure.
- Track actions and review trends: use incidents, near misses, maintenance data and audits to update assessments.
- Control change: require safety review before modifying machinery, software, tooling, materials, layout or production speed.
For new equipment purchases, safety should enter the specification stage rather than the commissioning stage. Guarding, access, lockout points, emergency stops, ergonomics, noise control, dust collection and maintenance clearance are easier to address before a machine is installed than after production depends on it.
Common gaps in industrial health and safety systems
The most common weaknesses are rarely caused by a lack of slogans. They are usually caused by a weak connection between the documented system and the work as performed.
- Procedures do not match field conditions: workers adapt informally because the written method is impractical.
- Risk assessments stop at normal production: cleaning, jam clearing and troubleshooting are missed even though they may carry higher exposure.
- Corrective actions focus on retraining: the same issue returns because the underlying design, access or planning problem remains.
- Change is not controlled: a production improvement introduces new pinch points, stored energy, exposure or maintenance access problems.
- Contractors are treated separately: outside workers may face unfamiliar equipment while site employees assume controls are understood.
- Audits check documents only: paperwork is complete, but guards, sensors, permits and isolation points are not verified in use.
Closing these gaps requires managers to ask a harder question: what would prove that the control works when production is busy, the machine is down, a contractor is waiting or a supervisor is under schedule pressure?
Frequently asked questions
Are health and safety systems the same as safety devices?
No. Safety devices such as guards, interlocks, emergency stops and gas detectors are parts of the overall control environment. A health and safety system is broader. It includes how hazards are identified, how controls are chosen, who maintains them, how workers are trained, how incidents are investigated and how the organization improves over time.
Is ISO 45001 required for every industrial site?
ISO 45001 is a voluntary international management system standard unless a customer, contract or local requirement makes it necessary. Many sites use it because it provides a structured, auditable framework. However, legal obligations still depend on the jurisdiction and the specific work being performed.
How often should risk assessments be reviewed?
There is no single interval that fits every workplace. Reviews should occur after incidents, near misses, equipment modifications, process changes, new materials, layout changes, contractor changes or evidence that controls are not working. Many organizations also schedule periodic reviews for high-risk equipment even when no event has occurred.
What is the strongest sign that a safety system is improving?
A strong sign is not simply a lower injury rate. Better evidence includes hazards reported early, critical controls verified regularly, corrective actions that remove root causes, workers involved in procedure design and management decisions that favor reliable controls over short-term convenience.