How Can Automation Systems Make Industrial Equipment More Reliable in 2026?
Why Does Automation Matter for Industrial Equipment Buyers?
Automation now has a real place in many industrial equipment buying decisions. If you buy machines for packaging, metal processing, food production, assembly, or material handling, you are not only buying steel, motors, and a control cabinet. You are also buying repeatable work, usable data, service access, and fewer guesses on the shop floor. For more related industrial system topics, you can browse the automation systems category.
Robot Adoption Shows a Durable Factory Shift
The change is easy to see from public data. The International Federation of Robotics reported in World Robotics 2025 that 542,076 industrial robots were installed worldwide in 2024, the second highest annual count in history. The same report listed 4,663,698 operational industrial robots at the end of 2024, up 9% from the prior year. This does not mean every plant needs a robot arm right away. It means buyers now expect equipment to connect, repeat, record, and run with less manual handling.
Repeatable Work Creates the Clearest Payback
Automation usually works best when the task is steady, dull, risky, or simple to define. A case packer that repeats the same movement all shift is often a better first project than a repair bench with changing parts and operator judgement. McKinsey Global Institute estimated in 2017 that 64% of global manufacturing work hours had technical automation potential with demonstrated technology. That number shows potential, not a guaranteed result. For a buyer, the better question is direct: which task wastes paid time every day?
Better Data Makes Equipment Easier to Sell
Data is now part of the machine package. Buyers often ask for cycle counts, alarm history, downtime reasons, reject totals, and energy use. A machine with a clear production record is easier to manage, easier to service, and easier to explain to finance. It also helps export buyers, because remote support can start from real records instead of a late-night photo of a fault light.
Which Factory Problems Should Automation Solve First?
Good automation does not start with a polished cabinet or the newest screen. It starts with one production problem that everyone can see. If you choose the wrong problem, the system may still run, but operators may work around it and maintenance may not trust it. Then management starts asking why the payback is slower than planned.
Bottleneck Machines Before Nice-to-Have Features
Start where the line waits. A filling machine that starves a labeler, a press brake with jobs queued in front of it, or a pallet station that blocks finished goods can all create visible cost. The first automation project should protect the bottleneck, not dress up the easy part of the line. In many factories, a simple infeed, outfeed, or reject handling upgrade can bring more value than a full cell built around the wrong machine.
Quality Checks Close to the Process
Inspection should sit near the point where defects begin. Machine vision after sealing, weighing after filling, torque checks after assembly, and barcode reading before packing can stop bad product before it moves downstream. This matters in export manufacturing, where one mixed carton can turn into a customer claim across an ocean. The fix may be small, but it can prevent a long and costly argument.
Labor Gaps and Safer Tasks
Labor pressure is another common reason to automate. Good targets are jobs that are repetitive, heavy, hot, sharp, dusty, or hard to staff on night shifts. The point is not only to replace hands. It is also to reduce fatigue and make the work more consistent. A lifting assist, servo pusher, or guarded transfer device may look simpler than a six-axis robot, but it can remove the worst task from a shift.
What Parts Make a Practical Automation System?
An automation system is not one magic box. It is a group of parts that must act like one machine. Layout, controls, sensors, safety devices, software, and service planning all affect the result. A neat electrical cabinet is useful, but a system that recovers cleanly after a jam is worth more on a busy floor.
Sensors, PLCs, and Motion Hardware
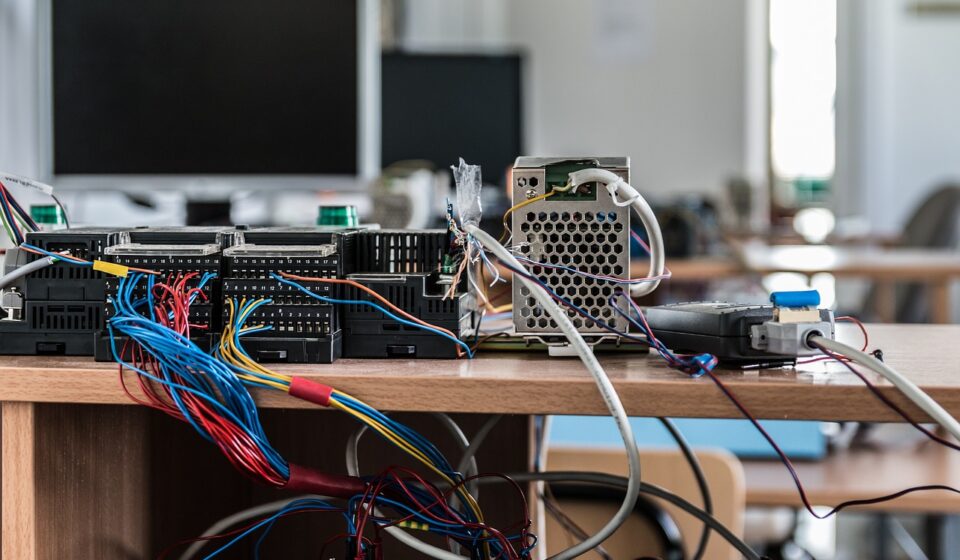
Sensors tell the system what is present, missing, full, open, closed, too fast, or out of position. PLCs handle the logic. Servo motors, drives, pneumatics, and actuators create the movement. For industrial equipment, these parts must fit the plant environment. A washdown food line, dusty cement packing area, and clean electronics station all need different sensor housings, cable routes, and cabinet ratings.
HMI, SCADA, and Data Records
The HMI should help operators run the machine without digging through confusing menus. Clear alarms, recipe names, manual controls, and maintenance screens reduce calls during shift change. SCADA or plant data links can track output, downtime, and trends across several machines. Keep the data useful. Most supervisors would rather see the three main downtime causes than a dashboard with fifty colors.
Grippers, Conveyors, and Machine Guards
Mechanical details often decide whether automation feels smooth or troublesome. A gripper must handle real product, not only perfect catalog samples. Conveyors need the right back pressure, guides, and cleaning access. Guards should protect people while still letting maintenance reach wear parts. If a guard needs fifteen bolts for a two-minute cleaning task, someone on the floor will start to dislike the design.
How Should You Compare Automation Equipment Suppliers?
Supplier choice affects the machine long after the purchase order is signed. A low price may look good at the start, but unclear scope, weak documents, and hard-to-find spare parts can cost more over the next three years. Compare proof, not only promises.
Proven Cycle Time and Stable Output
Ask for real cycle time under normal product conditions. Sample runs should include normal variation, not only perfect parts from a demo table. If a supplier claims 60 pieces per minute, ask what happens after a film roll change, box size change, or upstream stop. Reliable automation is boring in a good way. It keeps giving the same result when people are tired and the floor is busy.
Clear Integration Scope
Integration scope should say who supplies conveyors, robots, PLC programming, safety validation, air preparation, power wiring, network settings, and operator training. Many disputes come from gaps between the machine builder, robot integrator, and plant engineering team. A good proposal states what is included and what is excluded. It also tells the buyer what must be ready before installation.
Service Access and Spare Parts
Check the service plan before paying the deposit. Standard PLC brands, available sensors, labeled wiring, drawings, backups, and remote support options all help reduce downtime. For export buyers, spare parts packaging and part numbers matter a lot. One small proximity sensor can stop a large line if nobody knows the correct replacement. See also: buying guides.
How Can Automation Reduce Risk Instead of Adding It?
Automation can reduce risk, but safety and cybersecurity must be planned from the start. A fast machine with weak guarding is not an improvement. A connected line with loose access control also creates problems. Good design protects people, product, and data without making the machine hard to run.
Safety by Design
OSHA stated in its 2024 Work-Related Injury and Illness Summary that there are no specific OSHA standards for workplace robotics, while general rules such as lockout/tagout and machine guarding still apply. OSHA also identified 550 robot-related incidents in U.S. manufacturing narrative data for 2024; 33% were treated in an emergency room and 2% led to inpatient hospitalization. The message is plain. Risk assessment, guarding, interlocks, safe stops, and lockout points are not just paperwork. They are part of the machine.
OT Security for Connected Plants
Connected equipment gives plants remote support and better reporting, but it also needs access control. NIST SP 800-82 Rev. 3 gives guidance for operational technology security, including industrial control systems, PLCs, SCADA, and distributed control systems. NIST Cybersecurity Framework 2.0, released in 2024, also gives companies a wider method to manage cyber risk. For automation buyers, this means asking about user roles, backups, patch handling, network separation, and remote access approval.
Training That Fits Real Operators
Training should match the people who use the machine every day. Operators need startup, stop, changeover, jam clearing, and alarm response. Maintenance needs fault tracing, sensor replacement, lubrication points, backups, and safe recovery. A thick manual can help, but a laminated quick guide near the HMI often saves a shift. Use direct language and clear steps. People remember the sequence better than theory.
What Should You Measure After Installation?
After startup, you need numbers that show whether the system is doing its job. Do not measure everything just because the software can collect it. Pick the few numbers tied to money, safety, delivery, and customer complaints.
OEE, Scrap, and Changeover Time
Overall equipment effectiveness, scrap rate, and changeover time give a useful first view. If output rises but scrap also rises, the project is not finished. If the machine runs well on one size but loses forty minutes on every changeover, recipe control or tooling may need more work. Watch the first month closely, because small setup habits can become permanent faster than expected.
Energy Use and Maintenance Signals
Servo load, air consumption, motor current, temperature, vibration, and cycle counts can warn maintenance before a hard stop. These signals are useful for pumps, presses, compressors, conveyors, and packaging machines. You do not need a large predictive system on day one. Start by recording the signals linked to common failures and spare parts.
Payback With Room for Downtime
Payback should include uptime, scrap, labor redeployment, maintenance, training, utilities, spare parts, and support. Leave room for commissioning time. A new automation cell may need product tuning, operator habit changes, and small mechanical adjustments before it reaches stable output. That is normal in real production. Good projects plan for that curve instead of treating the first day as the final result.
FAQ
Q1: What Is the Best First Automation Project for a Factory? A: The best first project is usually a repeatable bottleneck with clear downtime, labor, scrap, or safety cost. Start with a task that can be measured before and after installation.
Q2: Does Automation Always Require Robots? A: No. Automation can use conveyors, sensors, PLC controls, vision systems, feeders, actuators, or simple fixtures. A robot is only one tool in the wider automation toolbox.
Q3: How Can You Check if an Automation Supplier Is Reliable? A: Ask for real cycle tests, clear scope, electrical drawings, spare parts lists, safety design details, and support response plans. A reliable supplier explains limits as clearly as benefits.
Q4: What Public Sources Support Automation Investment Decisions? A: Useful sources include the International Federation of Robotics World Robotics 2025 report, OSHA 2024 workplace injury summary, McKinsey Global Institute automation research, NIST OT security guidance, and ISA/IEC 62443 cybersecurity standards.
Q5: How Long Does Automation Payback Usually Take? A: Payback varies by machine, labor rate, downtime, scrap, product mix, and shift pattern. If reliable public data is not available for your exact process, use your own line data instead of a generic market claim.