How to choose material handling conveyors for safer throughput
Material handling conveyors are flow decisions, not just equipment purchases
Material handling conveyors move products, packages, pallets or bulk materials through a facility with less manual carrying, pushing and forklift travel. The right choice is rarely the fastest belt or the lowest quoted price. It is the system that fits the load, route, accumulation needs, safety requirements, maintenance capacity and future automation plan.
For warehouses, factories, distribution centers and processing sites, material handling conveyors should be evaluated as part of a wider material handling strategy: how goods arrive, where they pause, how they are inspected or sorted, and where they leave the process.
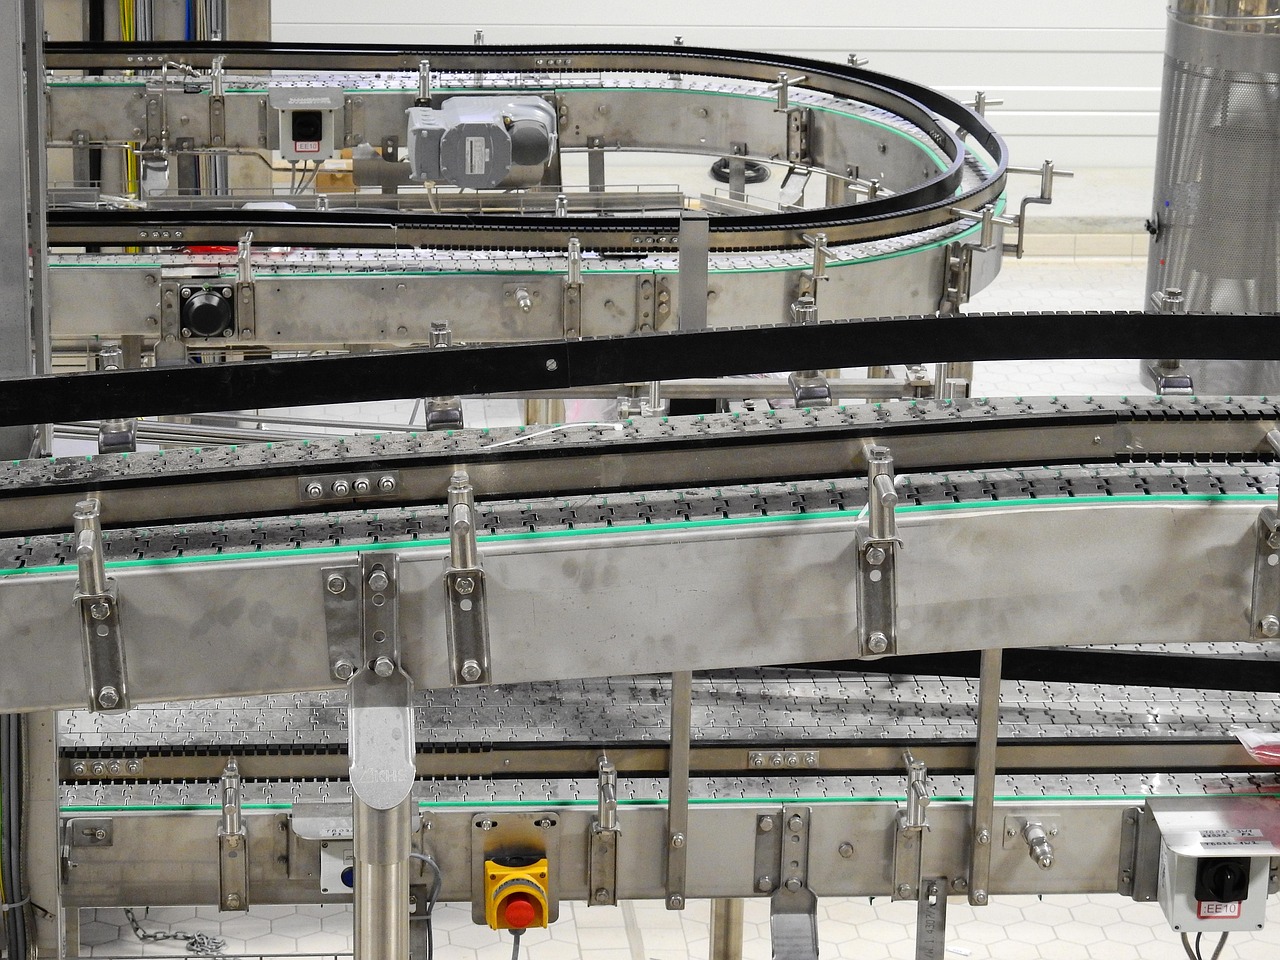
This guide covers the main conveyor types, practical selection criteria, safety standards buyers should know, and automation trends affecting conveyor design. The focus is decision quality, because many conveyor problems start with unclear assumptions about throughput, product variation or maintenance access.
What material handling conveyors do best
Conveyors are most valuable when material moves along a repeatable route at predictable volumes. They can reduce walking time, stabilize work pacing, connect process steps and provide fixed points for scanning, weighing, labeling, inspection or sortation. In high-volume operations, conveyors often become the backbone linking receiving, picking, packing, production, storage and shipping.
They are less suitable when routes change frequently, product sizes fall outside the conveyor design envelope, or the facility needs maximum layout flexibility. In those situations, carts, forklifts, autonomous mobile robots, tugger trains or hybrid systems may be more practical. A conveyor project should therefore begin with the movement problem, not the equipment catalog.
Useful questions include: What items need to move? How heavy are they? How often do they arrive? Do they need to accumulate? Will people work next to the line? Are there curves, inclines, transfers or elevation changes? Does the system need to connect with a warehouse management system, machine controls, sorters, robotics or packaging equipment?
Main conveyor types and where they fit
No single conveyor type fits every industrial operation. The table below summarizes common options and the conditions where they usually make sense.
| Conveyor type | Typical use | Key selection limits |
|---|---|---|
| Belt conveyor | Cartons, parcels, bags, packaged goods and some bulk materials | Belt material, incline angle, tracking, cleaning and product stability |
| Gravity roller conveyor | Manual packing, staging and short carton movement | Requires slope or manual force; not ideal for precise pacing |
| Powered roller conveyor | Carton transport, accumulation and zone control | Roller spacing, load bottom quality and control logic |
| Motor-driven roller conveyor | Zero-pressure accumulation and modular warehouse lines | Best for defined load ranges; requires electrical and controls planning |
| Chain conveyor | Pallets, heavy loads, fixtures and industrial work-in-process | Load support, lubrication, guarding and transfer design |
| Slat or apron conveyor | Assembly, hot parts, heavy components and harsh environments | Higher cost and maintenance compared with lighter systems |
| Screw conveyor | Powders, grains, chips and many bulk solids | Material flow behavior, abrasion, contamination control and cleaning |
| Spiral or vertical conveyor | Moving cartons or totes between elevations | Throughput, footprint, product stability and maintenance access |
| Sortation conveyor | Parcel, e-commerce, postal and order fulfillment operations | Data accuracy, induction rate, chute design and exception handling |
The critical factor is the product interface. A tote with a flat base behaves differently from a polybag, a pallet, a steel casting or a dusty bulk material. Product dimensions, center of gravity, surface friction, fragility and contamination risk can all change the correct conveyor choice.
Selection criteria that affect real system performance
Load data and product variation
Reliable conveyor design starts with a load profile, not an average. Buyers should document minimum and maximum length, width, height and weight; bottom condition; temperature; moisture; dust; oil; fragility; and the percentage of loads outside the normal range. A conveyor that works for 95 percent of items can still create daily jams if the remaining 5 percent are ignored.
Throughput and accumulation
Throughput should be expressed in units per hour, cartons per minute, pallets per hour or tons per hour, depending on the operation. Peak periods matter more than the daily average. If picking, packing, labeling or truck loading creates bursts, the system may need accumulation zones, buffering, merge control or bypass routes. Zero-pressure accumulation can protect cartons from contact damage, while controlled release can reduce downstream congestion.
Layout and transfer points
Many conveyor problems occur at transfers rather than on straight runs. Curves, merges, diverts, inclines, declines and elevation changes must be designed around the actual item mix. Small items may fall between rollers if spacing is wrong. Tall cartons may tip on inclines. Pallets may require chain transfers, turntables or lift-and-transfer modules. Maintenance access, emergency access and cleaning clearance should be considered before the layout is fixed.
Controls and software integration
Modern conveyors are increasingly controlled systems rather than passive mechanical lines. Photoeyes, encoders, programmable logic controllers, variable frequency drives, motor-driven roller zones, scanners and warehouse control software can determine whether the line runs smoothly. If a conveyor supports shipping sortation or automated replenishment, data quality is as important as mechanical capacity. A misread barcode or poorly timed divert can create a bottleneck even when the conveyor has enough mechanical speed.
Environment and maintenance capacity
Food, pharmaceutical, cold storage, mining, woodworking and metalworking environments create different design requirements. Cleaning, corrosion resistance, dust management, washdown needs, bearing protection and belt material should be matched to the site. Maintenance staffing also matters. A technically advanced system that cannot be inspected, cleaned and repaired by the available team will lose performance over time.
Safety and compliance points to validate early
Conveyors create pinch points, nip points, shear points, moving belts, rotating shafts, stored energy and falling-object risks. Safety should be addressed during concept design, not added after installation. In the United States, OSHA machine-guarding requirements under 29 CFR 1910.212 and hazardous-energy control requirements under 29 CFR 1910.147 are commonly relevant to conveyor operation and servicing. These rules do not replace a site-specific safety review, but they help define the basic duty to protect workers from machine hazards and unexpected energization.
ASME lists B20.1-2024 as the active Safety Standard for Conveyors and Related Equipment. Its stated scope covers conveyor design, construction, installation, maintenance, inspection and operation in relation to hazards, including bulk material, package and unit-handling conveyor systems. CEMA safety resources also emphasize practical tools such as safety labels, label placement guidance, emergency-stop application, conveyor crossovers, spill guarding and supplemental guarding.
For buyers and facility managers, the practical checklist should include guarding at nip points and drives, safe access around elevated sections, emergency-stop placement, lockout/tagout procedures, warning labels, safe cleaning methods, training for operators and maintenance workers, and documented inspection routines. Where conveyors interface with robotics, forklifts or manual workstations, the safety review should cover the full interaction zone rather than the conveyor alone. See also: production equipment.
Automation trends changing conveyor decisions
Conveyor projects are increasingly shaped by automation goals. MHI and Deloitte’s 2026 Annual Industry Report framed supply chain technology investment around the move from isolated tools toward connected, end-to-end operations. For conveyor buyers, the practical implication is that a conveyor should not be judged only by feet per minute. It should also be judged by how well it shares data, supports automation and adapts to changing order profiles.
Several trends are especially relevant:
- Motor-driven roller zones: These systems can reduce unnecessary running time and support controlled accumulation compared with continuously running lines.
- Smarter sensing: Photoeyes, scanners, weigh scales and condition-monitoring sensors help detect jams, spacing errors, belt misalignment and equipment wear earlier.
- Robotic interfaces: Conveyors increasingly feed robotic palletizers, depalletizers, piece-picking cells and packaging stations, which makes precise product positioning more important.
- Hybrid automation: Some facilities combine fixed conveyors for high-volume corridors with mobile robots or manual carts for variable routes.
- Energy and maintenance visibility: Drives, zones and controls can provide operating data that supports preventive maintenance and energy management.
These trends do not mean every facility needs a highly automated conveyor network. They do mean that even a basic conveyor purchase should consider future controls, data and expansion needs. A low-cost line that cannot integrate with scanning, sortation or zone control may become expensive if the facility later automates around it.
Common mistakes to avoid
The first mistake is designing around average demand. Conveyor systems are stressed during peaks, SKU changes, labor gaps and exception handling. A stronger design process models the busiest hour, the awkward load and the worst transfer point.
The second mistake is underestimating change. E-commerce, manufacturing schedules and distribution networks can shift quickly. Modular conveyor sections, adjustable supports, spare controls capacity and documented wiring can make future changes easier.
The third mistake is treating safety as a final inspection item. Guarding, access, emergency stops, crossovers and lockout points can affect layout, cost and productivity. Early safety planning usually reduces rework.
The fourth mistake is ignoring downtime recovery. A conveyor that stops a whole operation needs clear jam-clearing procedures, spare parts, maintenance access and bypass options. Throughput is not just how fast the system runs when everything is perfect; it is how reliably it recovers when something goes wrong.
A practical buyer checklist
- Define the load profile with minimum, maximum and exception cases.
- Calculate peak throughput, not only daily average volume.
- Map every transfer, merge, divert, incline and elevation change.
- Decide whether accumulation is required and where it should occur.
- Confirm safety guarding, emergency stops, access and lockout/tagout expectations.
- Check whether the conveyor must integrate with scanners, WMS, WCS, PLCs, robots or packaging equipment.
- Review cleaning, dust, temperature, corrosion and environmental requirements.
- Plan maintenance access, spare parts and operator training before commissioning.
- Allow room for expansion, rerouting or additional automated modules.
Frequently asked questions
What is the difference between material handling conveyors and general conveyors?
Material handling conveyors are conveyors used within the broader movement, storage and control of goods in industrial or logistics operations. The term usually refers to conveyors that move cartons, totes, pallets, parts or bulk materials between receiving, production, storage, picking, packing and shipping processes.
Are belt conveyors better than roller conveyors?
Neither is universally better. Belt conveyors support a wide range of item shapes and can handle smaller or irregular packages more easily. Roller conveyors are often efficient for cartons, totes and pallets with stable bottoms, especially where accumulation or modular zone control is needed. The load base, weight, speed, transfer design and maintenance needs should determine the choice.
When should a facility consider motor-driven roller conveyors?
Motor-driven roller conveyors are worth considering when the operation needs controlled accumulation, lower noise, modular zones or the ability to run only selected sections. They are common in carton and tote handling, but the item weight range, roller spacing and controls architecture must be checked before selection.
What standards should be considered for conveyor safety?
In the United States, OSHA rules on machine guarding and hazardous-energy control are commonly relevant. ASME B20.1-2024 is a major conveyor safety standard, and CEMA publishes industry safety resources for conveyor labels, guarding topics and safe application practices. A qualified safety professional should review the actual installation because requirements depend on the equipment, workers and site conditions.
How can conveyors support future warehouse automation?
Conveyors can provide consistent product flow, spacing, scanning locations and handoff points for sorters, robots, packaging machines and warehouse control systems. To support future automation, buyers should plan for sensors, controls capacity, data integration, modular expansion and safe access from the beginning.