Material handling in warehouse operations from equipment choices to safer workflows
Why material handling in warehouse operations needs a systems view
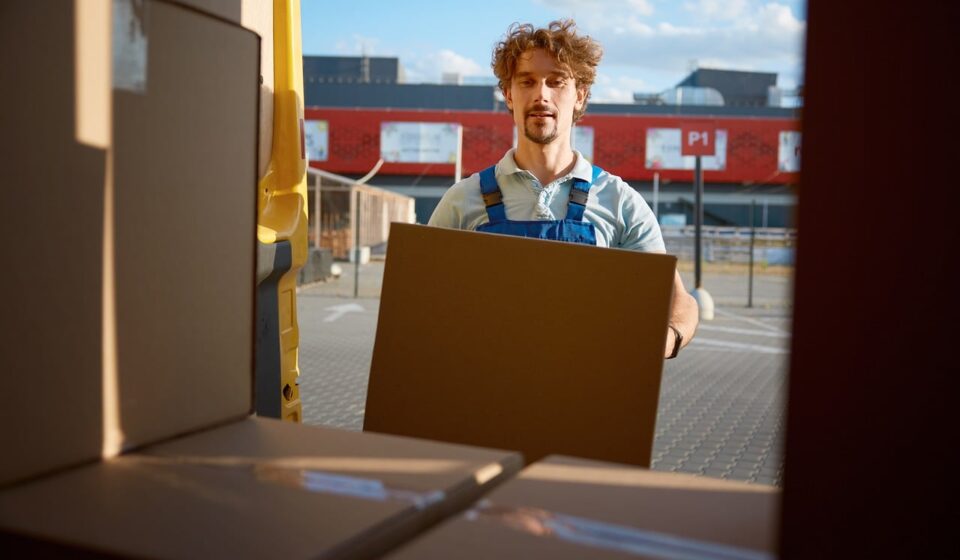
Material handling in warehouse operations is more than moving pallets with forklifts. It covers the decisions that determine how goods are received, moved, stored, picked, packed, staged and shipped while people, vehicles, racks, conveyors and software work in the same space. A well-designed system cuts unnecessary touches, travel distance, product damage, congestion and physical strain. A weak one adds hidden cost through rework, blocked aisles, unsafe stacking, inventory errors and equipment conflicts.
Labor and safety data underline the need for careful planning. The U.S. Bureau of Labor Statistics reported a 2024 total recordable injury and illness rate of 4.8 cases per 100 full-time workers for warehousing and storage, along with 32 fatalities in that subsector in 2024. OSHA identifies common warehousing hazards that include powered industrial trucks, ergonomics, material handling, slips and trips, hazardous chemicals and robotics. For operators, the handling plan has to improve flow and control risk at the same time.
What material handling includes inside a warehouse
In a warehouse, material handling covers the short-distance movement, storage, control and protection of goods. The work starts before a load reaches storage. Receiving teams unload trailers, verify quantities, inspect condition, identify goods and move them to a staging or putaway location. From there, the handling plan determines whether items go into pallet rack, shelving, floor storage, automated storage, pick modules or forward-pick locations.
The same system then supports replenishment, order picking, value-added work, packing, sortation and outbound staging. Every step changes the cost profile. A case may be unloaded, staged, moved to reserve storage, replenished to a pick face, picked again, conveyed to packing and staged for shipping. Reducing one touch at a high-volume point can be more valuable than buying a faster truck for a low-volume aisle.
Readers can find related industrial equipment and warehouse flow topics in the material handling category.
Map the flow before selecting equipment
Equipment decisions are often made too early. A warehouse may buy lift trucks, conveyors or mobile robots before it has defined the load profile, order pattern, storage density, travel path and labor constraint. A better first step is a flow map that follows each product family from inbound dock to outbound dock.
Useful mapping questions include:
- Which SKUs, pallets, cartons or totes create the most movement?
- Where do items wait, and why do they wait there?
- How many times is the same unit touched before it ships?
- Which aisles or dock doors create recurring congestion?
- Where do people and powered equipment cross paths?
- Which products drive damage, mispicks, overexertion or awkward lifting?
This mapping step also separates average flow from peak flow. Many warehouses run acceptably on a normal day but struggle during receiving surges, seasonal promotions, carrier cutoffs or inventory count periods. Equipment sized only for the average day can push workers toward shortcuts during peaks. Equipment sized only for the worst day, however, may tie up capital and floor space for months.
Common equipment choices and where they fit
The right equipment depends on the handling pattern. Forklifts are flexible, but they are not always the lowest-risk or lowest-cost answer. Conveyors are efficient for repeatable paths, but they can become expensive obstacles if the process changes often. Automated systems can reduce walking and manual handling, but they require stable data, disciplined maintenance and clear exception handling.
| Warehouse task | Common equipment | Main advantage | Key limitation |
|---|---|---|---|
| Trailer unloading and receiving | Dock levelers, pallet jacks, forklifts, conveyors | Moves goods quickly from dock to staging | High conflict risk if staging lanes and pedestrian paths are unclear |
| Pallet storage and replenishment | Counterbalance trucks, reach trucks, pallet rack, flow rack | Balances storage density with access | Requires rack capacity control, aisle clearance and trained operators |
| Case and each picking | Carts, pick modules, conveyors, voice systems, AMRs | Can reduce walking and improve pick sequence | Needs accurate slotting, inventory data and clear work methods |
| Workstation handling | Lift tables, tilters, hoists, turntables, adjustable benches | Reduces bending, reaching and awkward postures | Must match load size, cycle frequency and operator access |
| Outbound packing and sortation | Scales, dimensioners, conveyors, sorters, staging lanes | Improves shipping accuracy and carrier readiness | Can create bottlenecks if exceptions are not routed separately |
A practical equipment review should consider load weight and dimensions, travel distance, lift height, turning radius, floor condition, battery or fuel requirements, maintenance access and operator visibility. For storage systems, rack layout and load labels should be treated as operating controls, not background infrastructure.
Safety and compliance constraints that shape layout
Warehouse material handling is directly affected by safety rules and recognized industry practices. OSHA 29 CFR 1910.176 requires safe clearances where mechanical handling equipment is used, clear and properly maintained aisles, and secure storage that does not create a hazard. OSHA 29 CFR 1910.178 covers powered industrial trucks and requires operator training based on truck type, workplace hazards and general safe operation principles.
Ergonomics also matters because many warehouse injuries are not dramatic single events. OSHA describes ergonomic risk factors in warehousing such as lifting and lowering heavy items, bending, overhead reaching, pushing, pulling, awkward postures and repetitive work. NIOSH guidance on manual material handling and the Revised NIOSH Lifting Equation can help safety professionals evaluate defined lifting tasks, although those tools should be applied by qualified personnel and not treated as a universal weight limit.
Rack safety is another control point. The Rack Manufacturers Institute identifies ANSI MH16.1-2023 as the standard for design, testing and utilization of industrial steel storage racks. In practical terms, warehouse teams should know the rated capacity, inspect for damaged uprights and beams, control modifications and remove unsafe rack locations from service until they are reviewed.
As of OSHA information available in 2026, inspections under the updated National Emphasis Program on Warehousing and Distribution Center Operations began on July 31, 2026. The basic message for operators remains the same: aisle markings, training records, equipment inspections, rack condition and ergonomic risk controls should be visible in daily work, not only in written procedures. See also: production equipment.
How data and automation change the handling plan
Modern material handling depends increasingly on data. A warehouse management system, barcode scanning, RFID, sensors or a warehouse execution layer can improve the timing of moves and reduce search time. Software, however, cannot fix a poor physical layout by itself. If the pick face is badly slotted, replenishment rules are unclear or inventory accuracy is weak, automation may only move errors faster.
The MHI and Deloitte 2025 Annual Industry Report, released on March 19, 2025 and based on more than 700 supply chain leader responses collected at the end of 2024, shows why companies are looking closely at technology. The report said 55% of surveyed leaders had increased supply chain technology and innovation budgets. It also reported that 45% planned to purchase automated solutions and 42% planned to buy forklift trucks and other handling equipment. Surveyed leaders expected strong five-year adoption for inventory and network optimization, cloud computing, sensors, predictive analytics, robotics and automation.
For warehouse operators, the lesson is not that every facility should automate immediately. The stronger lesson is that data, equipment and workforce planning are now linked. Automation works best when it is tied to a measurable problem, such as excessive walking, poor replenishment timing, high sortation labor, limited floor space or heavy repetitive handling.
A practical improvement framework
Improving material handling does not always require a new building or a large automation project. Many facilities can make meaningful gains through a structured review:
- Measure current movement. Track touches, travel distance, dock-to-stock time, pick rate, replenishment delays, damage and near misses.
- Stabilize housekeeping and storage. Clear aisles, mark staging zones, control overhanging loads and keep emergency routes open.
- Separate people and equipment where possible. Use marked walkways, crossing points, mirrors, barriers, speed controls and traffic rules appropriate to the site.
- Improve slotting before buying more equipment. Move high-velocity items closer to pick and ship points, and place heavy or awkward items at safer handling heights.
- Match equipment to the repeatable task. Use lift assists, tilters or conveyors where repetitive strain is the issue; use trucks or AMRs where travel and flexible routing are the issue.
- Build inspection routines into work. Include forklifts, pallet jacks, dock equipment, conveyors, rack damage, guards and floor conditions.
- Train for the actual workplace. Generic training is not enough if the site has narrow aisles, mixed pedestrians, unusual loads, mezzanines, battery charging areas or automated equipment.
The strongest programs treat warehouse handling as a living system. SKU mix changes, order profiles change, labor availability changes and equipment ages. A layout that worked three years ago may now create congestion because e-commerce each picking has grown, pallets are taller or carrier pickup windows have tightened.
Frequently asked questions
What is material handling in a warehouse?
It is the movement, storage, control and protection of goods inside the warehouse, from receiving and putaway through picking, packing, staging and shipping. It includes manual work, powered equipment, storage systems, conveyors, workstations and supporting data systems.
What equipment is most common for warehouse material handling?
Common equipment includes forklifts, pallet jacks, reach trucks, pallet racks, shelving, conveyors, carts, lift tables, hoists, dock levelers, sorters and automated mobile robots. The right mix depends on load size, travel distance, storage height, order pattern, throughput and safety constraints.
How can a warehouse improve material handling without full automation?
Start with layout, slotting, aisle discipline, staging rules and ergonomic aids. Reducing unnecessary touches, improving pick-face design, adding lift-assist equipment and separating pedestrian routes from powered equipment can deliver improvements before a major automation project is justified.
Is warehouse automation always the best answer?
No. Automation is most effective when the process is measurable, repeatable and supported by accurate inventory data. If demand is unstable, SKU data is poor or exceptions are frequent, a phased approach may be safer: fix process discipline first, then automate the highest-value movement or handling bottleneck.
Which safety issues should be reviewed first?
Begin with powered industrial truck traffic, blocked or narrow aisles, unstable storage, damaged racks, poor dock controls and repetitive manual lifting. These issues affect both productivity and worker risk, so they should be part of the same improvement plan rather than separate projects.
Final takeaway
Material handling in warehouse operations works best when equipment, layout, people, storage and information are planned together. The goal is not simply to move goods faster. The goal is to move the right goods with fewer touches, safer methods, better visibility and enough flexibility to handle real warehouse variation.